

Types of Ceramic Materials: Classification, Properties & Applications
Ceramic materials are inorganic, non-metallic materials with unique combinations of mechanical, thermal, electrical, and chemical properties. Depending on their composition, structure, and manufacturing process, ceramics can provide advantages such as high temperature resistance, excellent hardness, electrical insulation, corrosion resistance, and wear resistance.
Ceramic materials can be classified in different ways. By composition, the main types include oxide, carbide, nitride, boride, silicate, and glass-ceramic materials. Ceramics can also be divided into traditional and advanced ceramics according to their raw materials, manufacturing control, and performance requirements. These two systems describe different aspects of the same material. For example, alumina is both an advanced ceramic and an oxide ceramic.
Among these categories, advanced ceramics such as alumina (Al₂O₃), aluminum nitride (AlN), silicon carbide (SiC), silicon nitride (Si₃N₄), and zirconia (ZrO₂) are widely used in electronics, semiconductor manufacturing, aerospace, medical devices, and industrial components.
This guide introduces the major types of ceramic materials, their key properties, and typical applications.
Classification of Ceramic Materials by Composition
Based on composition, ceramic materials can be classified into oxide ceramics, nitride ceramics, carbide ceramics, boride ceramics, silicate ceramics, and glass ceramics.
| Ceramic Category | Examples | Key Characteristics | Common Applications |
| Oxide Ceramics | Alumina, Zirconia, MgO, SiO₂ | High temperature resistance, chemical stability, electrical insulation | Electronics, medical, industrial components |
| Nitride Ceramics | AlN, Si₃N₄, BN | High thermal conductivity, strength, thermal shock resistance | Semiconductor, aerospace, high-temperature systems |
| Carbide Ceramics | SiC, B₄C, WC | Extreme hardness, wear resistance, high-temperature performance | Wear parts, abrasives, armor |
| Boride Ceramics | TiB₂, ZrB₂ | Ultra-high temperature stability, hardness | Cutting tools, aerospace |
| Silicate Ceramics | Porcelain, Mullite, Cordierite | Low cost, insulation, traditional ceramic properties | Construction, electrical insulation |
| Glass and Glass-Ceramics | Fused silica, lithium aluminosilicate glass-ceramics | Low thermal expansion, optical properties | Cookware, optics |
Oxide Ceramics
Oxide ceramics are ceramic materials where oxygen is the primary anion combined with metallic elements. They are known for high melting points, chemical stability, electrical insulation, and wear resistance.
Common oxide ceramics include:
- Alumina (Al₂O₃)
- Zirconia (ZrO₂)
- Silica (SiO₂)
- Magnesia (MgO)
Typical applications include:
- Electronic components
- Electrical insulators
- Medical devices
- High-temperature components
Carbide Ceramics
Carbide ceramics, including silicon carbide (SiC) and boron carbide (B₄C), are known for high hardness, wear resistance, and performance in demanding thermal and mechanical environments. Silicon carbide is widely used in seals, heat exchangers, semiconductor components, and furnace parts, while boron carbide is used in abrasives, blasting nozzles, wear components, and lightweight protective systems.
Nitride Ceramics
Nitride ceramics include aluminum nitride (AlN), silicon nitride (Si₃N₄), and boron nitride (BN), but these materials serve different purposes. AlN is mainly selected for thermal conductivity and electrical insulation, Si₃N₄ for mechanical strength and thermal shock resistance, and BN for electrical insulation, low friction, thermal stability, and machinability.
Boride Ceramics
Boride ceramics, such as titanium diboride (TiB₂) and zirconium diboride (ZrB₂), provide high hardness, electrical conductivity, wear resistance, and high-temperature capability. They are used in conductive ceramic components, molten-metal systems, cutting tools, and selected ultra-high-temperature applications.
Silicate Ceramics
Silicate ceramics are mainly composed of silicon and oxygen compounds, including aluminosilicates and magnesium silicates. They are among the most traditional ceramic materials and are widely used due to their availability, durability, and cost-effectiveness.
Common silicate ceramics include:
- Mullite
- Cordierite
- Porcelain
- Steatite
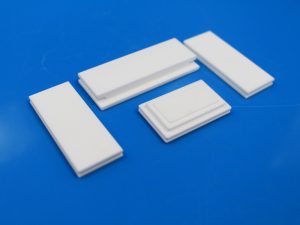
Mullite is commonly used in furnace and kiln components because of its high-temperature stability. Cordierite is valued for low thermal expansion and thermal shock resistance, while porcelain and steatite are widely used in electrical insulation and general industrial components.
Further Reading: What are Silicate Ceramics
Glass and Glass-Ceramics
Glass ceramics are produced by controlled crystallization of glass materials, combining characteristics of both glass and ceramics. Glass is primarily amorphous, while glass-ceramics contain controlled crystalline phases produced through heat treatment.
They typically offer:
- Low thermal expansion
- Good thermal stability
- Optical properties
Applications include:
- Cookware
- Optical components
- Heat-resistant products
Traditional Ceramics vs. Advanced Ceramics
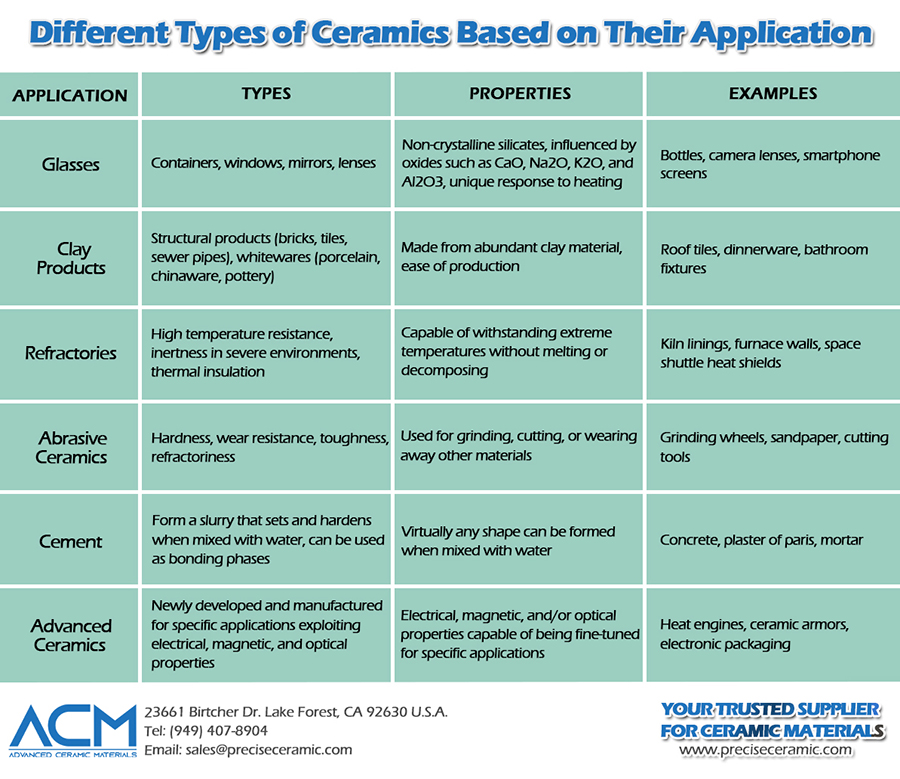
Ceramic materials can also be broadly divided into traditional and advanced ceramics according to their raw materials, manufacturing control, and performance requirements. Traditional ceramics are mainly used in construction and daily products, while advanced ceramics are engineered for demanding industrial and high-performance applications.
Traditional Ceramics
Traditional ceramics are mainly produced from natural raw materials such as clay, silica, and feldspar.
Common examples include:
- Bricks
- Tiles
- Porcelain
- Cement-based ceramic products
Advanced Ceramics
Advanced ceramics are engineered materials manufactured from high-purity compounds such as alumina, silicon carbide, silicon nitride, aluminum nitride, and zirconia. Compared with traditional ceramics, advanced ceramics are designed for demanding applications requiring superior mechanical strength, thermal performance, electrical properties, or chemical stability.
They provide superior properties including:
- High temperature resistance
- High hardness
- Electrical insulation
- Thermal conductivity
- Chemical resistance
Applications include:
- Semiconductor manufacturing
- Aerospace components
- Electronic packaging
- Medical devices
- Industrial wear components
Further Reading: An Overview of Advanced Ceramic Materials
Common Advanced Ceramic Materials and Applications
The following are some of the most widely used advanced ceramic materials and their typical properties and applications.
Alumina (Al₂O₃)
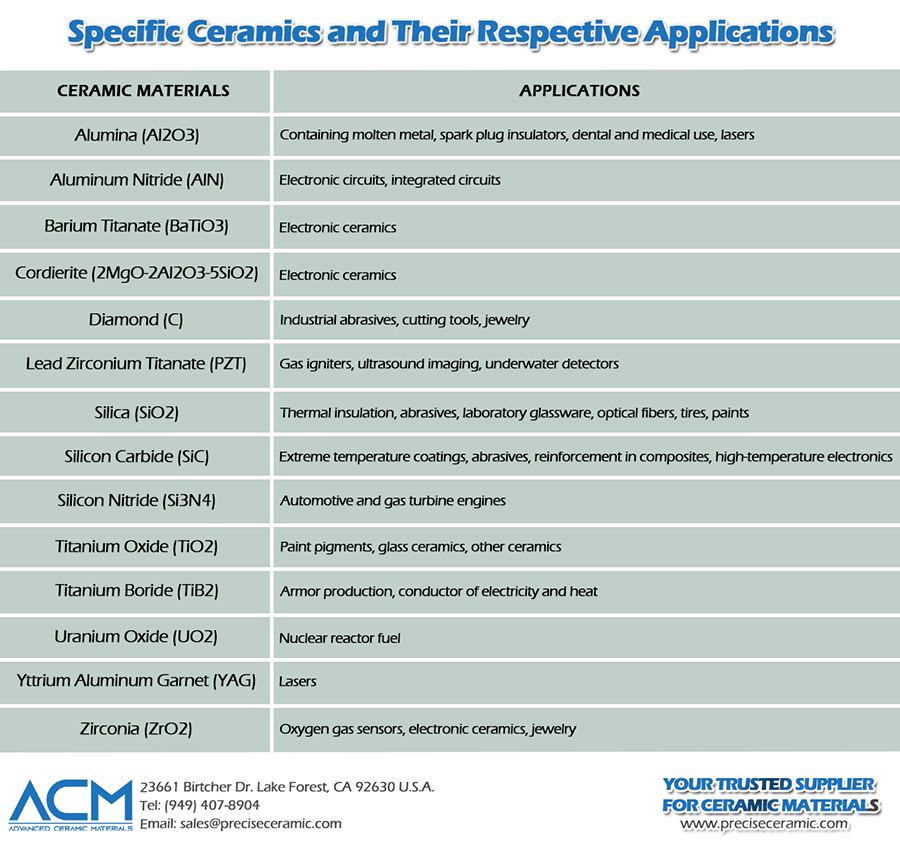
Alumina (Al₂O₃) is one of the most widely used advanced ceramic materials due to its excellent electrical insulation, high hardness, wear resistance, chemical stability, and high-temperature performance. Available in a wide range of purity grades, alumina ceramics can be tailored for different mechanical, electrical, and industrial requirements.
Common applications include:
- Semiconductor components
- Electrical insulators
- Ceramic substrates
- Wear-resistant parts
- Laboratory crucibles
- High-temperature components
Typical commercial alumina grades range from approximately 85% to 99.9% purity, with higher-purity alumina providing improved mechanical strength, chemical resistance, and electrical performance.
Aluminum nitride (AlN)
Aluminum nitride (AlN) is an advanced ceramic material known for its excellent thermal conductivity combined with electrical insulation. Its thermal expansion coefficient is close to silicon, making it particularly suitable for electronic packaging and semiconductor applications.
Common applications include:
- Semiconductor substrates
- LED heat dissipation components
- Power electronic modules
- High-frequency electronic devices
Aluminum nitride typically provides thermal conductivity of 140–180 W/m·K and electrical resistivity above 10¹⁴ Ω·cm.
Silicon Carbide (SiC)
Silicon carbide is known as one of the best ceramic materials for very high-temperature applications. It combines excellent hardness, wear resistance, thermal conductivity, corrosion resistance, and thermal shock resistance.
Common applications include:
- Mechanical seals
- Heat exchangers
- Semiconductor components
- Abrasives
- High-temperature structural parts
Silicon Nitride (Si₃N₄)
Silicon nitride is a high-performance technical ceramic known for its excellent mechanical strength, fracture toughness, thermal shock resistance, and chemical stability. Compared with many ceramic materials, it offers a strong balance between strength and thermal performance.
Common applications include:
- Bearings
- Engine components
- High-temperature parts
- Semiconductor processing components
Zirconia (ZrO₂)
Zirconia (ZrO₂) is a high-performance ceramic material known for its excellent fracture toughness, strength, wear resistance, and chemical stability. Compared with many traditional ceramics, zirconia provides superior resistance to crack propagation, making it suitable for applications requiring durability and reliability.
Common applications include:
- Medical and dental ceramics
- Precision components
- Wear-resistant parts
- Oxygen sensors
- Structural ceramic components
Zirconia is often selected when higher toughness and impact resistance are required compared with alumina ceramics.
Boron Nitride (BN)
Boron nitride is an advanced ceramic material known for its excellent thermal stability, electrical insulation, chemical resistance, and low friction properties. Hexagonal boron nitride (h-BN) is widely used in thermal management and high-temperature applications.
Common applications include:
- Thermal management components
- High-temperature insulation
- Lubricants
- Semiconductor processing
Titanium Boride (TiB₂)
Titanium diboride (TiB₂) is an ultra-high-temperature ceramic known for its high hardness, excellent wear resistance, and good electrical and thermal conductivity. It is suitable for demanding environments requiring mechanical durability and thermal stability.
Common applications include:
- Armor materials
- Cutting tools
- High-temperature components
- Molten metal applications
Silica (SiO₂)
Silicon dioxide is an essential ingredient in many engineering ceramics and thus is the most widely used ceramic material. Silica-based materials are used in thermal insulation, abrasives, laboratory glassware, etc. It also found application in communications media as an integral part of optical fibers. Fine particles of silica are used in tires, paints, etc.
How to Choose an Advanced Ceramic Material
| Primary Requirement | Recommended Material | Main Reason |
|---|---|---|
| General electrical insulation | Alumina | Balanced performance, availability, and cost |
| High thermal conductivity with insulation | Aluminum Nitride | Transfers heat while remaining electrically insulating |
| High fracture toughness | Zirconia | Better resistance to crack propagation |
| Wear and thermal shock resistance | Silicon Carbide | Hardness, thermal conductivity, and thermal stability |
| Mechanical strength under thermal cycling | Silicon Nitride | Strength, toughness, and thermal shock resistance |
| Machinable high-temperature insulation | Boron Nitride | Electrical insulation and machinability |
| Extreme hardness with low density | Boron Carbide | Very high hardness and relatively low density |
Final material selection should also consider operating temperature, chemical exposure, mechanical loading, purity, component geometry, and dimensional tolerances.
Conclusion
Ceramic materials cover a wide range of compositions and applications, from traditional ceramics used in daily products to advanced ceramics designed for high-performance industrial applications.
Understanding the differences between oxide ceramics, non-oxide ceramics, silicate ceramics, and glass ceramics helps engineers select suitable materials based on mechanical, thermal, electrical, and chemical requirements.
Advanced Ceramic Materials (ACM) supplies alumina, aluminum nitride, silicon carbide, silicon nitride, zirconia, boron nitride, and other advanced ceramics in standard and custom forms. If you are comparing materials for a specific operating temperature, environment, or component design, contact us for material and manufacturing recommendations.

{{item.content}}
LEVE A REPLY
{{item.children[0].content}}
{{item.content}}
LEAVE A REPLY
SUBSCRIBE OUR NEWSLETTER
- Why Do Kilns Need Both SiC Plates and SiC Tubes?
- Ceramic vs. Metallic Heating Elements: A Technical Selection Guide for Design Engineers
- Ceramic Heating Coil Versus Cotton Coil: Choosing the Better Fit
- 5 Ways Alumina Ceramic Plates Keep Heavy Industry Running
- Oxide, Sulfide, or Phosphate? A Supplier's Guide to Solid-State Electrolyte Ceramics

 Ceramic Machining: Essential Techniques and Processes for Precise Components
This article explains ceramic machining in plain language. It covers how ceramic items are produced, the role of machining in shaping these products, and methods such as grinding, milling, and CNC machining.
READ MORE >
 Alumina Powder (Al2O3): A Technical Guide to Grades, Properties, and Applications
How to choose alumina powder purity from 92% to 99.99%. ACM guide covers decision tree, properties, ZTA, and application tables for engineers.
READ MORE >
 Ceramic Heating Coil Versus Cotton Coil: Choosing the Better Fit
When people compare a ceramic heating coil with a cotton coil, the real question is usually not "which one is better on paper?" It is "which one makes life easier in daily use?" In practice, that comes down to heat control, maintenance, lifespan, and how often you want to swap parts or deal with burnt taste.
READ MORE >