

Alumina Ceramics: Properties, Purity Grades, and Key Applications
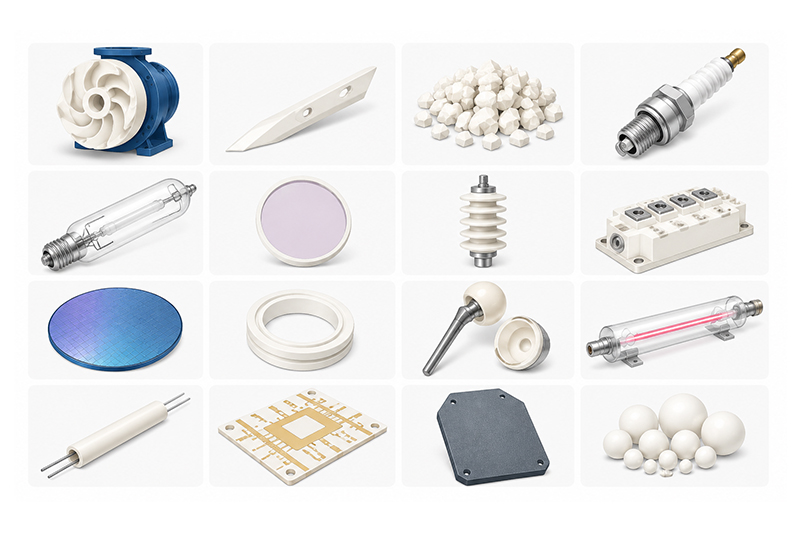
Alumina ceramic, also known as aluminum oxide ceramic (Al₂O₃), is one of the most widely used advanced oxide ceramics. It provides a practical combination of electrical insulation, hardness, wear resistance, chemical stability, high-temperature capability, and cost-effectiveness.
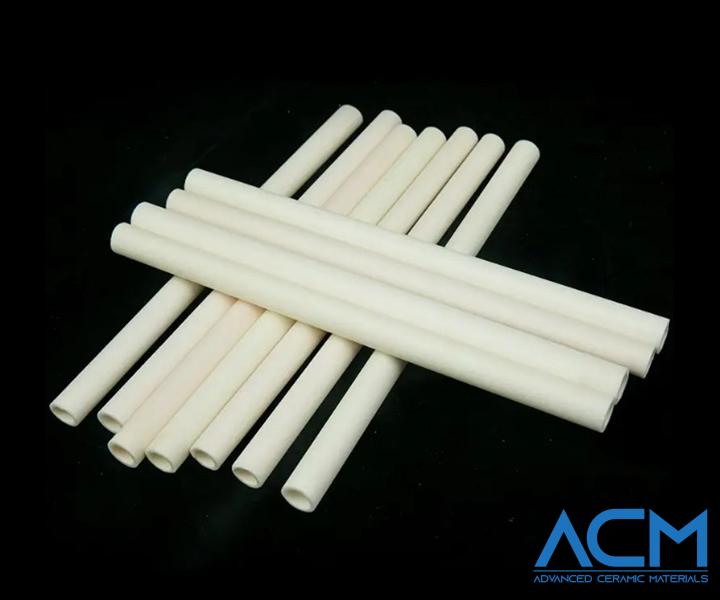
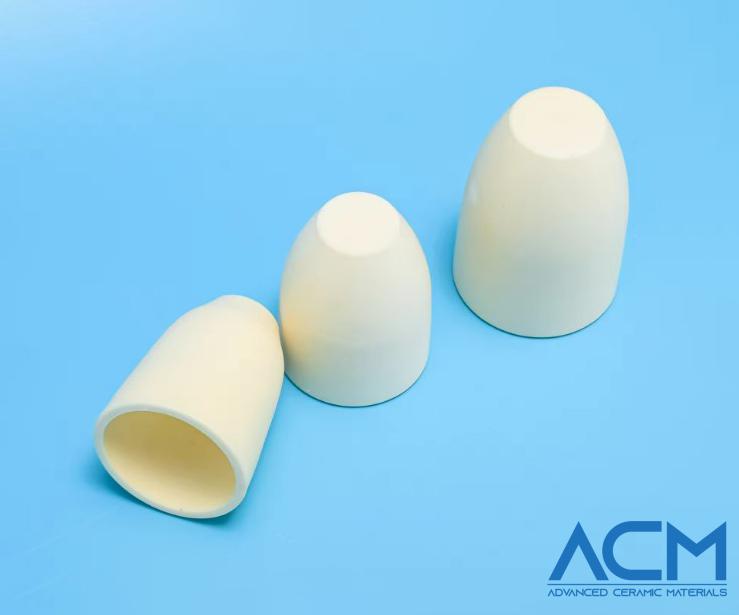
Alumina is available in different purity grades and product forms, including plates, tubes, rods, crucibles, substrates, grinding media, and custom components. This article explains its principal properties, manufacturing methods, purity grades, applications, and the factors to consider when selecting an alumina ceramic.
What Is Alumina Ceramic?
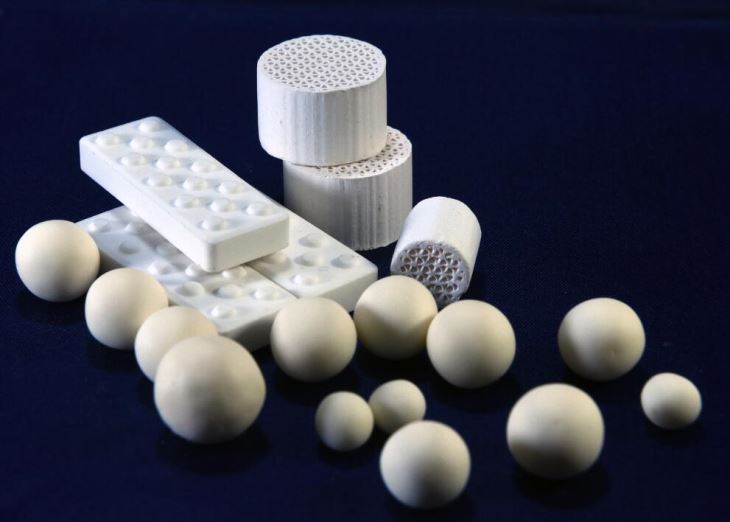
Alumina ceramic is an oxide ceramic made primarily from aluminum oxide (Al₂O₃). Most engineering alumina uses the stable alpha-alumina crystal structure, while small amounts of additives may be introduced to support densification or modify particular properties.
Industrial alumina powder is commonly produced by refining aluminum-bearing raw materials and is then processed into ceramic components. The powder can be formed by dry pressing, isostatic pressing, extrusion, injection molding, slip casting, or tape casting, depending on the required geometry and production volume. The formed component is subsequently debound and sintered to develop its final density and properties.
After sintering, critical dimensions and surface finishes can be produced through diamond grinding, lapping, or polishing. These are finishing processes rather than primary forming methods.
Alumina ceramics are used because they combine high hardness, electrical insulation, chemical resistance, stiffness, and relatively mature manufacturing processes. Their final performance depends on alumina purity, additives, porosity, grain size, forming method, sintering conditions, and surface quality.
Properties of Alumina Ceramics
Alumina ceramic properties vary with purity, additives, density, grain size, manufacturing process, and operating temperature. Published values should therefore be treated as grade-specific rather than as universal values for all alumina ceramics.
Mechanical Properties
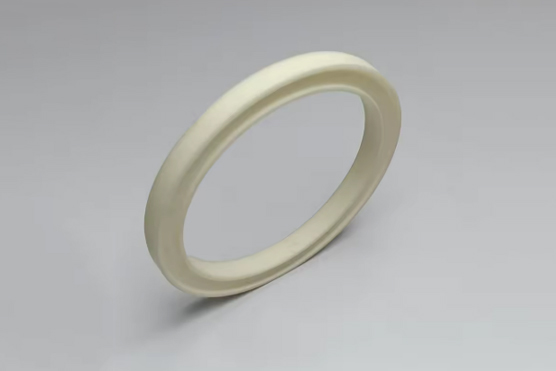
Alumina provides high hardness, stiffness, compressive strength, and resistance to abrasive wear. These properties make it suitable for seals, guides, liners, nozzles, grinding media, and other components exposed to friction or particle erosion.
Like most ceramics, alumina is brittle and is less tolerant of tensile stress, impact, sharp corners, and surface damage than ductile metals. Component geometry, mounting, surface finish, and load direction must therefore be considered during design.
Electrical Properties
Dense alumina is an excellent electrical insulator with high volume resistivity, useful dielectric strength, and relatively low dielectric loss. It is widely used in insulators, feedthroughs, substrates, ignition components, and electrical housings.
Electrical performance depends on purity, additives, porosity, frequency, temperature, and component thickness. Higher-purity alumina is often selected for demanding electrical and semiconductor applications, but final values should be confirmed using data for the specific grade.
Thermal Properties
Alumina remains stable at temperatures beyond the practical limits of most polymers and many metals. Its thermal conductivity is higher than that of zirconia but substantially lower than that of high-conductivity aluminum nitride and many silicon carbide grades.
Alumina can be used for high-temperature components, but maximum service temperature and thermal shock resistance depend on purity, geometry, atmosphere, heating rate, cooling rate, and mechanical loading. Thin or carefully designed components generally tolerate temperature changes better than thick components with abrupt section changes.
Chemical Properties
Alumina is insoluble in water and resists many corrosive environments. It is used in pump, valve, laboratory, semiconductor, and chemical-processing components where chemical stability and contamination control are important.
Its corrosion resistance is not universal. Strong acids, strong alkalis, molten salts, and high-temperature chemical environments may attack alumina depending on concentration, temperature, exposure time, purity, and grain-boundary composition.

Alumina Purity Grades: 95%, 99%, 99.5%, and 99.7%
Alumina purity influences density, electrical performance, chemical stability, temperature capability, manufacturability, and cost. Higher purity is not automatically necessary for every application; the most suitable grade is the one that meets the operating requirements without adding unnecessary processing expense.
| Alumina Grade | General Characteristics | Typical Starting Applications |
|---|---|---|
| 95% alumina | Cost-effective, strong, wear-resistant, and widely available | General insulators, wear parts, tubes, rods, spacers, and industrial components |
| 99% alumina | Improved purity, electrical properties, and chemical stability | Electrical components, laboratory parts, substrates, and higher-temperature applications |
| 99.5% alumina | Higher purity and tighter contamination control | Semiconductor equipment, high-voltage insulation, vacuum components, and analytical equipment |
| 99.7% alumina | High chemical purity and strong electrical and thermal stability | Demanding semiconductor, research, vacuum, and high-temperature components |
The figures above are general selection guidance. Actual properties depend on the manufacturer's formulation, additives, density, grain size, and production process. Applications involving vacuum, semiconductor processing, medical devices, or direct chemical contact may also require additional material certification and process control.
For a more detailed purity comparison table, please visit our alumina grades and product page.
Application of Alumina Ceramics
Electrical and Electronic Components
Alumina is widely used for electrical insulators, feedthroughs, ignition components, terminal supports, substrates, housings, and high-voltage components. It combines electrical insulation with mechanical strength, chemical stability, and resistance to elevated temperatures.
Higher-purity alumina is often selected when dielectric performance, low contamination, or stable behavior at elevated temperature is required.
Semiconductor and Vacuum Equipment
Alumina components are used in semiconductor-processing, vacuum, plasma, and analytical equipment. Typical parts include insulating rings, chambers, tubes, fixtures, feedthroughs, wafer-handling components, and custom-machined parts.
Material purity, porosity, surface finish, cleaning process, and dimensional tolerances are particularly important in these applications.
Wear and Fluid-Handling Components
The hardness and chemical resistance of alumina make it suitable for seal rings, valve components, pump parts, liners, guides, nozzles, and textile-processing components. Alumina is often selected when metal components experience excessive abrasion, corrosion, or contamination.
High-Temperature and Laboratory Components
Alumina crucibles, tubes, boats, thermocouple protection tubes, and furnace components are used in laboratories and industrial thermal processes. The appropriate purity and component design depend on temperature, atmosphere, sample chemistry, heating rate, and thermal cycling.
Automotive and Energy Applications
Alumina is used in spark-plug insulators, sensors, electrical isolation components, and selected power-electronic assemblies. In electric and hybrid vehicles, alumina components and substrates can provide electrical isolation, mechanical support, and thermal stability.
Transparent Alumina
Transparent or translucent alumina is used in selected optical windows, high-pressure lamps, protective optical components, and infrared systems. These applications require specialized control of purity, porosity, grain structure, and finishing, and should not be treated as equivalent to standard opaque alumina ceramic.
Further Reading: What is the Transparent Ceramic Material
When Should You Consider Another Ceramic?
Alumina is a practical general-purpose technical ceramic, but it is not the best choice for every requirement.
| If the Application Requires | Consider | Why |
|---|---|---|
| Higher fracture toughness or impact tolerance | Zirconia | Greater resistance to crack propagation |
| Much higher thermal conductivity with electrical insulation | Aluminum nitride | Better suited to demanding heat-spreading applications |
| Stronger thermal shock and corrosion performance | Silicon carbide | Useful in rapid thermal cycling and aggressive environments |
| Strength under repeated thermal and mechanical loading | Silicon nitride | Combines toughness, strength, and thermal shock resistance |
| Easier machining of complex high-temperature insulation | Boron nitride | More machinable than dense alumina |
The final choice should be based on the complete operating environment rather than a single property.
Conclusion
Alumina is one of the most versatile advanced ceramics because it combines electrical insulation, hardness, wear resistance, chemical stability, and high-temperature capability at a relatively practical cost. Its performance, however, varies with purity, additives, density, microstructure, manufacturing method, and component design.
Grades such as 95% alumina are suitable for many general industrial applications, while higher-purity grades may be required for semiconductor, vacuum, electrical, analytical, and contamination-sensitive systems.
Advanced Ceramic Materials (ACM) supplies alumina plates, tubes, rods, crucibles, substrates, grinding media, and custom components in multiple purity grades. Contact us with your required dimensions, operating temperature, environment, and drawing for material and manufacturing recommendations.
Further Reading: Ceramic Material Selection Made Easy: A Buyer's Guide to Key Properties

{{item.content}}
LEVE A REPLY
{{item.children[0].content}}
{{item.content}}
LEAVE A REPLY
SUBSCRIBE OUR NEWSLETTER
- Why Do Kilns Need Both SiC Plates and SiC Tubes?
- Ceramic vs. Metallic Heating Elements: A Technical Selection Guide for Design Engineers
- Ceramic Heating Coil Versus Cotton Coil: Choosing the Better Fit
- 5 Ways Alumina Ceramic Plates Keep Heavy Industry Running
- Oxide, Sulfide, or Phosphate? A Supplier's Guide to Solid-State Electrolyte Ceramics
 Ceramic Machining: Essential Techniques and Processes for Precise Components
This article explains ceramic machining in plain language. It covers how ceramic items are produced, the role of machining in shaping these products, and methods such as grinding, milling, and CNC machining.
READ MORE >
 Alumina Powder (Al2O3): A Technical Guide to Grades, Properties, and Applications
How to choose alumina powder purity from 92% to 99.99%. ACM guide covers decision tree, properties, ZTA, and application tables for engineers.
READ MORE >
 Ceramic Heating Coil Versus Cotton Coil: Choosing the Better Fit
When people compare a ceramic heating coil with a cotton coil, the real question is usually not "which one is better on paper?" It is "which one makes life easier in daily use?" In practice, that comes down to heat control, maintenance, lifespan, and how often you want to swap parts or deal with burnt taste.
READ MORE >